
联系我们1

当前位置:
上海 鹿程国际贸易(桂林市分公司) >桂林本地今日News
武汉50WH250价格
更新时间:2026-11-07 22:42:53 ip归属地:桂林,天气:小雨,温度:15-21 浏览次数:3 公司名称:上海 鹿程国际贸易(桂林市分公司)
以下是:广西省桂林市武汉50WH250价格的产品参数
| 产品参数 | |
|---|---|
| 产品价格 | 2/吨 |
| 发货期限 | 3天内 |
| 供货总量 | 50000 |
| 运费说明 | 电议 |
| 小起订 | 1 |
| 质量等级 | 精品 |
| 是否厂家 | 是 |
| 产品材质 | 冷轧 |
| 产品品牌 | 宝武日本进口 |
| 产品规格 | 0.08-0.65 |
| 发货城市 | 上海武汉 |
| 产品产地 | 上海武汉 |
| 加工定制 | 粗加工 |
| 产品型号 | 多种 |
| 可售卖地 | 全国 |
| 质保时间 | 一年 |
| 适用领域 | 电器马达电机变压器磁感器互感器稳压器继电器电磁开关新能源电机电动汽车变压器军工电机发电机组航天造船汽车等 |
| 是否进口 | 否 |
| 品名 | 电工钢 冷轧无取向电工钢 冷轧取向电工钢卷冷轧取向硅钢 取向电工钢冷轧无取向硅钢冷轧无取向硅钢 |
| 规格 | 0.08 0.1 0.05 0.18 0.2 0.23 0.27 0.3 0.35 0.5 0.65 1.0mm |
| 包装 | 原厂精包装 |
| 用途 | 电器马达电机变压器磁感器互感器稳压器继电器电磁开关新能源电机电动汽车变压器军工电机发电机组航天造船汽车等 |
| 范围 | 武汉50WH250价格供应范围覆盖广西省、桂林市、南宁市、柳州市、梧州市、北海市、钦州市、贵港市、玉林市、百色市、贺州市、河池市、来宾市、崇左市、防城港市 秀峰区、叠彩区、七星区、雁山区、阳朔县、临桂区、灵川县、全州县、永福县、灌阳县、资源县、平乐县、荔浦市等区域。 |
以下是:广西省桂林市武汉50WH250价格的图文视频




【鹿程】为客户提供多样化产品,包括叠彩硅钢、灌阳硅钢、南宁电工钢、河池汽车大梁钢、防城港电工钢、钦州新能源电工钢、柳州汽车大梁钢等,适配多元场景需求。武汉50WH250价格,鹿程国际贸易(桂林市分公司)为您提供武汉50WH250价格,联系人:鹿丙伟,电话:【052788266222】。 广西壮族自治区,桂林市 2022年,桂林市实现地区生产总值2435.75亿元。按可比价计算,比上年增长2.5%。
武汉50WH250价格的详细视频已经上传,从产品的外观到内在,从功能到性能,视频将为您呈现一个真实、的产品形象。
以下是:广西桂林武汉50WH250价格的图文介绍

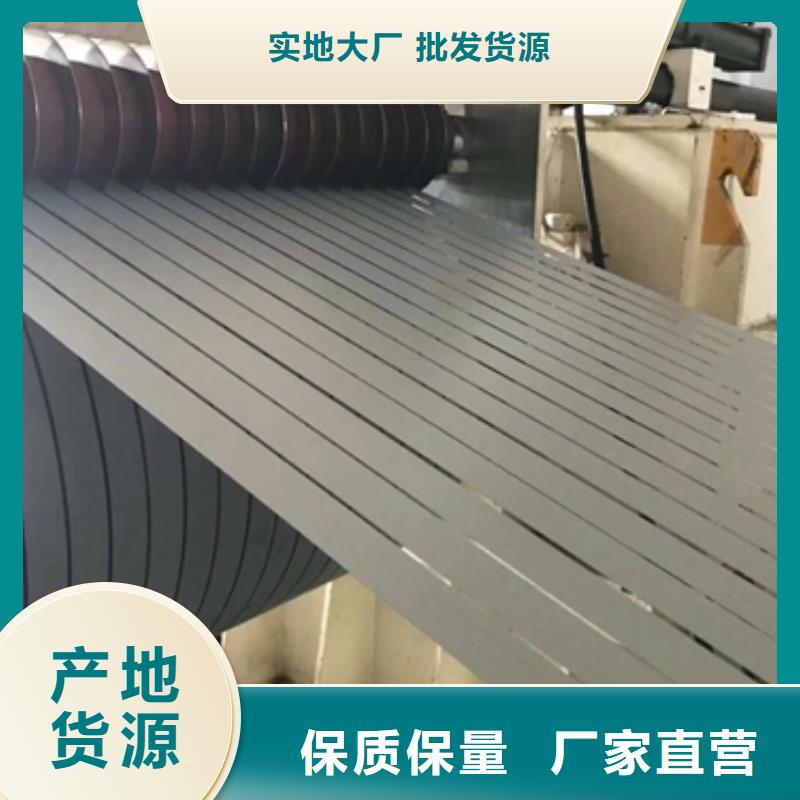
电工钢硅钢片Intro of iron core of automobile driving motor。At present, the motor technology of high-speed punching of stator and rotor iron core at home and abroad has developed rapidly. With the development of stamping equipment, new equipment with high quality, high efficiency and high precision has been provided for the production of motor punching pieces of high-speed punching of stator and rotor iron core at home and abroad, which has brought the motor punching process technology. Therefore, the design technology of new technology and equipment suitable for it has become a new research topic. The simultaneous separation of stator punching groove and stator punching groove of motor high-speed punching stator rotor iron core the simultaneous cutting of air gap between rotor punching and rotor punching groove is a new technological scheme applied to high-speed punching machine. This scheme has been widely used in foreign countries and has just begun research and application in domestic motor industry. Therefore, some discussions are made to realize the design technology of this technology according to the required technological equipment.The influence of motor high-speed punching of stator and rotor iron core: the influence of motor punching process technology of motor high-speed punching of stator and rotor iron core in new product development the traditional process of motor punching in our country is two categories: double punching and single punching, which are analyzed as follows:1) the process scheme of double punching groove: this scheme has good groove shape and uniformity, few processes and few tooling, but the tooling is complex and requires high precision, good equipment conditions, long tooling manufacturing cycle and Cheng Bengao, which is only suitable for mass production and is not conducive to new product development and small batch trial production.2) single-type punching process scheme: this scheme has poor groove shape, many processes, many tooling, many equipments, simple tooling, unstable quality, long production cycle and Cheng Bengao, and is only suitable for medium and small batch production.Requirements for high-speed punching of stator and rotor iron core of motor: 1. Positioning accuracy requirements. In this technological scheme, the two composite processes of punching groove separation and punching groove cutting air gap require the same positioning Benchmark, ensuring that the concentricity of the groove shape of the stator and rotor, the outer circular dove tail groove and shaft hole is not more than 0.02mm, the positioning of the center hole meets the technical requirements of concentricity, and the joint positioning of the small side hole and the center hole meets the requirements of circumferential orientation. 2. Precision requirements of composite process. Punching and groove separation compound process: This process has Groove-shaped convex mold and incision convex mold to complete the progressive blanking process. This process first punches and then cuts to separate the fixed and rotor punching pieces. The Two convex molds act synchronously on the same center track, and the central included angle between the two convex molds is one and a half times the central included angle of the groove. This process equipment is applied to high-speed punching machines, the groove-shaped indexing accuracy is guaranteed by the CAM stepping mechanism on the equipment;Electric vehicle is an economical and clean green vehicle based on electric drive,Environment and other aspects have * competitiveness, and can conveniently use modern control technology to realize its electromechanical integration, with broad development prospects.The motor drive system of the iron core of the automobile drive motor is the power source of the electric vehicle, and is the main body and internal basis for determining various performance indexes of the automobile operation. At present, electric vehicle motors mainly include DC motors, induction motors, permanent magnet brushless motors and switched reluctance motors.Automobile drive motor iron core permanent magnet brushless motor can be divided into two categories: one is permanent magnet synchronous motor with sine wave current,The other is the BLDC motor with rectangular pulse wave current.Two kinds of motors, the rotor is magnet, the motor rotor does not need brush and excitation winding, through stator winding commutation to generate rotating torque. Because the rotor has no excitation winding, no copper consumption, small magnetic flux and very small iron consumption at low load, therefore, the permanent magnet brushless motor has a high "Power/mass" ratio and can run at high speed. At the same time, it is easy to cool down because there is no abrasion of the rotor and the stator winding is the main heat source.The characteristics of the iron core of the automobile driving motor; The permanent magnet brushless motor of the iron core of the automobile driving motor has high reliability and high output power. Compared with other motors with the same rotating speed, it has the characteristics of small volume, light weight, easy maintenance, high efficiency, high power factor, etc. The rotor has small electromagnetic time constant and good dynamic characteristics of the motor. Through adjustment and conduction angle, constant power operation can be realized, and the efficiency of the motor can also be optimized by optimizing control angle, thus obtaining wider constant power operation area and higher efficiency.Overview of motor high speed punching stator and rotor iron core


鹿程国际贸易(桂林市分公司)生产的 硅钢产品销往全国十多个省、市、自治区,由于质量高、服务好、价格低,受到广大消费者的一致好评。我们本着“诚信经营、不断创新、顾客至上”的经营理念,在生产销售各种规格的 硅钢产品的同时还按照用户需求进行来图加工和来样加工,制造上述或其他产品。把企业着力打造成专业化程度高、服务好 硅钢生产厂家。


电工钢硅钢片硅钢是一种硅铁合金。用硅钢轧制的片材是电工领域中应用广的软磁材料,因而硅钢片又称电工钢片。硅钢片广泛用于电动机、发电机、变压器、扼流圈、电磁机构、继电器及测量仪表中电机工业大量使用厚度为0.35~0.50mm的硅钢片,用于:中型旋转机,压缩电机,通用马达,小型精密电机,电动汽车,压缩机,通用电机,电源变压器,精密变压器,节能电机,焊机变压器,稳压器,磁性密封器,加速器用电磁铁,汽车电机等;在电信高频技术中常用0.05~0.20mm的薄带钢片,以便更有效地降低涡流损耗。热轧硅钢片厚度为0.35~0.50mm,密度为7.55~7.70g/cm3,多用于大、中、小型交、直流电动机;冷轧无取向硅钢片厚度为0.35~0.50mm,密度为7.65~7.75g/cm3,多用于大型交流发电机、电动机,大、中、小型交、直流电动机;冷轧取向硅钢片厚度为0.23mm 0.27mm 0.3mm 0.35mm,密度为7.65g/cm3,多用于电力变压器、油浸式变压器,干式变压器,电抗器、磁放大器等;冷轧取向薄带厚度为0.05~0.20mm,多用于无线电高频变压器。


电工钢硅钢片自粘接涂层Z C3 C-3 - C-3涂层为有机成分,具有很高的层间电阻,并可以大幅提高钢带的冲片性能,很适合用于冲压叠片。用户使用时,先将钢板冲制成铁心叠片,然后加压固定成型,在保压条件下加热固化,叠片彼此粘接在一起,形成整体。其固定方式和常见的铆接、广西桂林同城焊接、广西桂林同城螺栓方式不同,刚度、广西桂林同城强度更高,振动和噪音小。涂层交货状态为 B 状态,即涂层还没有发生完全固化,具有进一步粘接、广西桂林同城固化的活性,涂层硬度、广西桂林同城耐蚀性尚没有达到 。涂层钢卷仓储有效期为半年。用户固化的工艺为:a)炉烘温度 160~230℃,模具压紧的压力为 0.3~3Mpa,时间保持1~3h;或 b)感应固化的铁心温度 150~250℃,压力 0.1~3MPa,时间保持 0.2~30min。固化后,涂层处于终稳定的状态,即 C 状态,涂层硬度、广西桂林同城强度、广西桂林同城粘接力达到 。涂层不能承受正常的应力退火温度。涂层能承受 180℃的长期耐热温度;但考虑到粘结能力的稳定性,适用于该涂层的工作温度通常不超过 150℃。

武汉50WH250价格,鹿程国际贸易(桂林市分公司)专业从事武汉50WH250价格,联系人:鹿丙伟,电话:【052788266222】,以下是武汉50WH250价格的详细页面。