
联系我们

当前位置:
上海 鹿程国际贸易(运城市分公司) >运城当地今日热点
35PN360电工钢带
更新时间:2026-10-10 06:19:46 ip归属地:运城,天气:多云,温度:11-27 浏览次数:3 公司名称:上海 鹿程国际贸易(运城市分公司)
以下是:山西省运城市35PN360电工钢带 的产品参数
| 产品参数 | |
|---|---|
| 产品价格 | 2/吨 |
| 发货期限 | 3天内 |
| 供货总量 | 50000 |
| 运费说明 | 电议 |
| 小起订 | 1 |
| 质量等级 | 精品 |
| 是否厂家 | 是 |
| 产品材质 | 冷轧 |
| 产品品牌 | 宝武日本进口 |
| 产品规格 | 0.08-0.65 |
| 发货城市 | 上海武汉 |
| 产品产地 | 上海武汉 |
| 加工定制 | 粗加工 |
| 产品型号 | 多种 |
| 可售卖地 | 全国 |
| 质保时间 | 一年 |
| 适用领域 | 电器马达电机变压器磁感器互感器稳压器继电器电磁开关新能源电机电动汽车变压器军工电机发电机组航天造船汽车等 |
| 是否进口 | 否 |
| 品名 | 电工钢 冷轧无取向电工钢 冷轧取向电工钢卷冷轧取向硅钢 取向电工钢冷轧无取向硅钢冷轧无取向硅钢 |
| 规格 | 0.08 0.1 0.05 0.18 0.2 0.23 0.27 0.3 0.35 0.5 0.65 1.0mm |
| 包装 | 原厂精包装 |
| 用途 | 电器马达电机变压器磁感器互感器稳压器继电器电磁开关新能源电机电动汽车变压器军工电机发电机组航天造船汽车等 |
| 范围 | 35PN360电工钢带 供应范围覆盖山西省、太原市、大同市、长治市、晋城市、阳泉市、朔州市、晋中市、运城市、忻州市、临汾市、吕梁市 盐湖区、临猗县、万荣县、闻喜县、稷山县、新绛县、绛县、垣曲县、夏县、平陆县、芮城县、永济市、河津市等区域。 |
以下是:山西省运城市35PN360电工钢带 的图文视频




【鹿程】以匠心打造多元场景产品,涵盖临猗汽车钢、万荣汽车大梁钢、新绛冲压用钢、垣曲新能源电工钢、平陆硅钢、忻州汽车车轮用钢、阳泉新能源电工钢、朔州汽车车轮用钢等。35PN360电工钢带 ,鹿程国际贸易(运城市分公司)为您提供35PN360电工钢带 的资讯,联系人:鹿丙伟,电话:【052788266222】。 山西省,运城市 运城市,简称“运”,古称河东,别称凤凰城,山西省辖地级市,位于山西西南部,北依吕梁山与临汾接壤,东峙中条山和晋城毗邻,西、南分别与陕西渭南、河南三门峡隔黄河相望,介于东经110°15'—112°04',北纬34°35'—35°49'之间,东西长201.87千米,南北宽127.47千米,总面积14182平方千米。截至2022年10月,运城市辖1个市辖区、2个县级市、10个县。截至2022年末,运城市常住人口为471.85万人。
为了让您更地了解我们的35PN360电工钢带 ,我们精心制作了产品视频。请花1分钟时间观看,您会发现更多细节和优势。
以下是:山西运城35PN360电工钢带 的图文介绍


电工钢硅钢片硅钢是一种硅铁合金。用硅钢轧制的片材是电工领域中应用广的软磁材料,因而硅钢片又称电工钢片。硅钢片广泛用于电动机、发电机、变压器、扼流圈、电磁机构、继电器及测量仪表中电机工业大量使用厚度为0.35~0.50mm的硅钢片,用于:中型旋转机,压缩电机,通用马达,小型精密电机,电动汽车,压缩机,通用电机,电源变压器,精密变压器,节能电机,焊机变压器,稳压器,磁性密封器,加速器用电磁铁,汽车电机等;在电信高频技术中常用0.05~0.20mm的薄带钢片,以便更有效地降低涡流损耗。热轧硅钢片厚度为0.35~0.50mm,密度为7.55~7.70g/cm3,多用于大、中、小型交、直流电动机;冷轧无取向硅钢片厚度为0.35~0.50mm,密度为7.65~7.75g/cm3,多用于大型交流发电机、电动机,大、中、小型交、直流电动机;冷轧取向硅钢片厚度为0.23mm 0.27mm 0.3mm 0.35mm,密度为7.65g/cm3,多用于电力变压器、油浸式变压器,干式变压器,电抗器、磁放大器等;冷轧取向薄带厚度为0.05~0.20mm,多用于无线电高频变压器。


我厂坐落于宝山区蕰川公路777号宝钢厂区607-609室,交通条件便利,技术实力雄厚,经济后盾强大,市场前景广阔。鹿程国际贸易(运城市分公司)生产设备齐全,配套能力强,有一整套严格的【硅钢】生产管理体系和质量保证体系并拥有一支素质良好的员工队伍,在【硅钢】产品的生产方面,已形成一整套独特可靠的工艺流程与生产方法,【硅钢】产品规格齐全,价格合理、客户至上、服务周到、让利客户、薄利多销为原则,诚实守信为宗旨。经过多年的经营,已经同全国各厂家建立了稳固的供货体系,同使用单位建立了良好的经营体系。 公司愿与各地的新老客户共同搭起一座智慧的桥梁!与您共同发展灿烂美好的明天!


电工钢硅钢片Intro of iron core of automobile driving motor。At present, the motor technology of high-speed punching of stator and rotor iron core at home and abroad has developed rapidly. With the development of stamping equipment, new equipment with high quality, high efficiency and high precision has been provided for the production of motor punching pieces of high-speed punching of stator and rotor iron core at home and abroad, which has brought the motor punching process technology. Therefore, the design technology of new technology and equipment suitable for it has become a new research topic. The simultaneous separation of stator punching groove and stator punching groove of motor high-speed punching stator rotor iron core the simultaneous cutting of air gap between rotor punching and rotor punching groove is a new technological scheme applied to high-speed punching machine. This scheme has been widely used in foreign countries and has just begun research and application in domestic motor industry. Therefore, some discussions are made to realize the design technology of this technology according to the required technological equipment.The influence of motor high-speed punching of stator and rotor iron core: the influence of motor punching process technology of motor high-speed punching of stator and rotor iron core in new product development the traditional process of motor punching in our country is two categories: double punching and single punching, which are analyzed as follows:1) the process scheme of double punching groove: this scheme has good groove shape and uniformity, few processes and few tooling, but the tooling is complex and requires high precision, good equipment conditions, long tooling manufacturing cycle and Cheng Bengao, which is only suitable for mass production and is not conducive to new product development and small batch trial production.2) single-type punching process scheme: this scheme has poor groove shape, many processes, many tooling, many equipments, simple tooling, unstable quality, long production cycle and Cheng Bengao, and is only suitable for medium and small batch production.Requirements for high-speed punching of stator and rotor iron core of motor: 1. Positioning accuracy requirements. In this technological scheme, the two composite processes of punching groove separation and punching groove cutting air gap require the same positioning Benchmark, ensuring that the concentricity of the groove shape of the stator and rotor, the outer circular dove tail groove and shaft hole is not more than 0.02mm, the positioning of the center hole meets the technical requirements of concentricity, and the joint positioning of the small side hole and the center hole meets the requirements of circumferential orientation. 2. Precision requirements of composite process. Punching and groove separation compound process: This process has Groove-shaped convex mold and incision convex mold to complete the progressive blanking process. This process first punches and then cuts to separate the fixed and rotor punching pieces. The Two convex molds act synchronously on the same center track, and the central included angle between the two convex molds is one and a half times the central included angle of the groove. This process equipment is applied to high-speed punching machines, the groove-shaped indexing accuracy is guaranteed by the CAM stepping mechanism on the equipment;Electric vehicle is an economical and clean green vehicle based on electric drive,Environment and other aspects have * competitiveness, and can conveniently use modern control technology to realize its electromechanical integration, with broad development prospects.The motor drive system of the iron core of the automobile drive motor is the power source of the electric vehicle, and is the main body and internal basis for determining various performance indexes of the automobile operation. At present, electric vehicle motors mainly include DC motors, induction motors, permanent magnet brushless motors and switched reluctance motors.Automobile drive motor iron core permanent magnet brushless motor can be divided into two categories: one is permanent magnet synchronous motor with sine wave current,The other is the BLDC motor with rectangular pulse wave current.Two kinds of motors, the rotor is magnet, the motor rotor does not need brush and excitation winding, through stator winding commutation to generate rotating torque. Because the rotor has no excitation winding, no copper consumption, small magnetic flux and very small iron consumption at low load, therefore, the permanent magnet brushless motor has a high "Power/mass" ratio and can run at high speed. At the same time, it is easy to cool down because there is no abrasion of the rotor and the stator winding is the main heat source.The characteristics of the iron core of the automobile driving motor; The permanent magnet brushless motor of the iron core of the automobile driving motor has high reliability and high output power. Compared with other motors with the same rotating speed, it has the characteristics of small volume, light weight, easy maintenance, high efficiency, high power factor, etc. The rotor has small electromagnetic time constant and good dynamic characteristics of the motor. Through adjustment and conduction angle, constant power operation can be realized, and the efficiency of the motor can also be optimized by optimizing control angle, thus obtaining wider constant power operation area and higher efficiency.Overview of motor high speed punching stator and rotor iron core

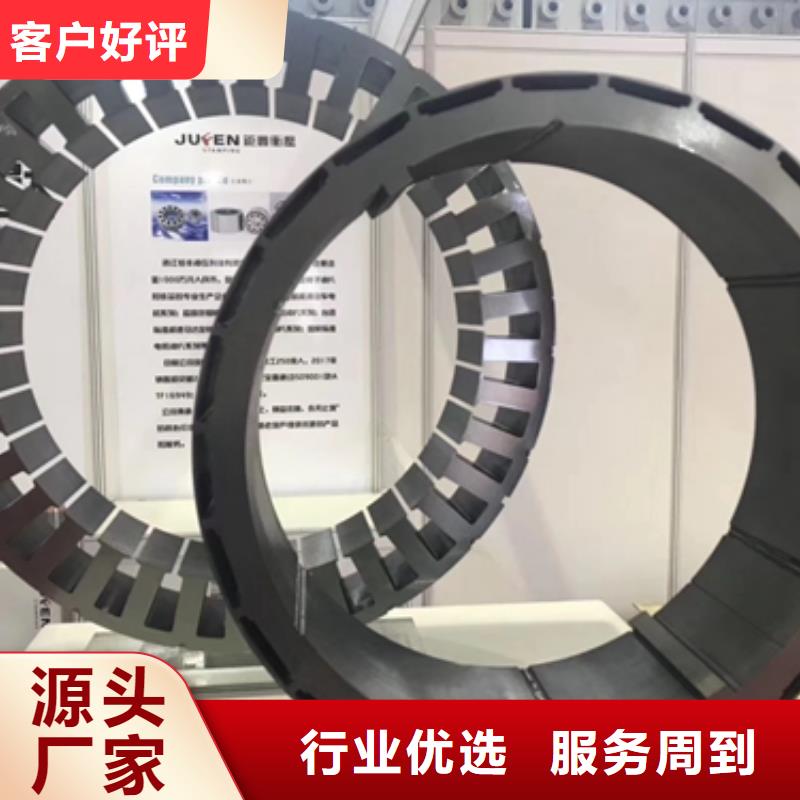

电工钢硅钢片我国太原钢铁厂于1952年首先试制热轧低硅钢板(1%~2%Si),1954年正式生产。1957年由钢铁研究总院研制成功3%Si冷轧取向硅钢,到1973年我国已掌握Armco技术 要点,鞍钢进行试制但未能生产。1974年武汉钢铁公司从日本新日铁引进冷轧取向硅钢制造装备和 。1976~1977年,钢铁研究总院在验证和消化日本 的基础上开发了Hi-B取向硅钢。1979年武钢正式生产取向硅钢,到目前为止武钢仍是我国取向硅钢的主要生产基地。


电工钢硅钢片硅钢是一种硅铁合金。用硅钢轧制的片材是电工领域中应用广的软磁材料,因而硅钢片又称电工钢片。硅钢片广泛用于电动机、发电机、变压器、扼流圈、电磁机构、继电器及测量仪表中电机工业大量使用厚度为0.35~0.50mm的硅钢片,用于:中型旋转机,压缩电机,通用马达,小型精密电机,电动汽车,压缩机,通用电机,电源变压器,精密变压器,节能电机,焊机变压器,稳压器,磁性密封器,加速器用电磁铁,汽车电机等;在电信高频技术中常用0.05~0.20mm的薄带钢片,以便更有效地降低涡流损耗。热轧硅钢片厚度为0.35~0.50mm,密度为7.55~7.70g/cm3,多用于大、中、小型交、直流电动机;冷轧无取向硅钢片厚度为0.35~0.50mm,密度为7.65~7.75g/cm3,多用于大型交流发电机、电动机,大、中、小型交、直流电动机;冷轧取向硅钢片厚度为0.23mm 0.27mm 0.3mm 0.35mm,密度为7.65g/cm3,多用于电力变压器、油浸式变压器,干式变压器,电抗器、磁放大器等;冷轧取向薄带厚度为0.05~0.20mm,多用于无线电高频变压器。
35PN360电工钢带 _鹿程国际贸易(运城市分公司),固定电话:【052788266222】,移动电话:【052788266222】,联系人:鹿丙伟,山西省运城市宝山区蕰川公路777号宝钢厂区607-609室。